

Creaform Ametek Freeform 3D Scanner Task Fit Routing for Industrial Measurement Teams
For most Western plants, the decision to research a Creaform Ametek freeform 3D scanner solution isn’t driven by a general interest in metrology.
Core Freeform 3D Scanning Task Classes for Industrial Use
Here is the section written from the perspective of a pre-sales solution consultant, tailored for Western industrial buyers and adhering to the strict constraints.
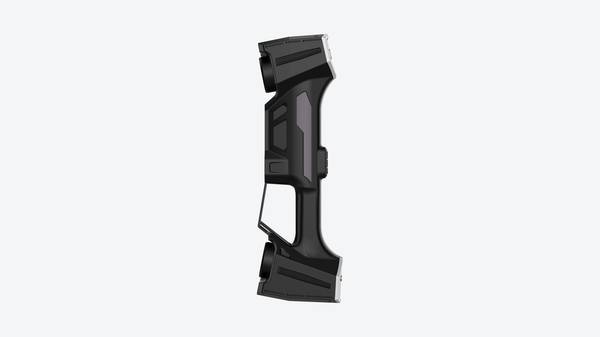
Practical Workflow
- Core Freeform 3D Scanning Task Classes for Industrial Use — Here is the section written from the perspective of a pre-sales solution consultant, tailored for Western industrial buyers and a…
- INSVISION Freeform 3D Scanning Portfolio Routing Logic — The core routing decision for any freeform scanning task comes down to four constraints: part size, site access, marker condition…
- Sample Validation Workflow for Freeform Scanning Fit Conf… — A structured validation workflow matters when you move from spec-sheet review to an actual purchase decision.
- Actionable Freeform 3D Scanner Pre-Qualification Checklist — Plain text, no markdown, 100–180 words, operational checklist angle, Western industrial buyer language.
For most Western plants, the decision to research a Creaform Ametek freeform 3D scanner solution isn’t driven by a general interest in metrology. It is triggered by three specific, high-friction task classes that traditional touch probing or hand tools cannot resolve efficiently. Routing the evaluation through these tasks—rather than raw specs—clarifies where the operational value sits.
Deployment Validation Checklist
| Focus Area | Decision Point | Deployment Note |
|---|---|---|
| Target part | Check size, surface condition, and key tolerances against the scan task | Run a full trial scan on a representative part |
| Data workflow | Verify point cloud, deviation map, and quality-report handoff | Confirm export formats and review ownership in advance |
| Shop-floor use | Review training, calibration, lighting, and working space | Keep the validation record as a repeatable inspection reference |
The first class is aerospace MRO freeform surface reverse engineering. Here, the deliverable is a CAD-compatible surface model of a worn, undocumented, or legacy airfoil or fairing. The second task is automotive OEM first-article inspection of contoured composite parts. These parts deflect under probe pressure, making CMM data noisy.
The required output is an ASME GD&T report showing deviation from nominal on complex curvature. The third class is medical device implant quality validation, where the scan data must support ISO 13485-aligned traceability without contaminating the part. Each of these tasks shares a common requirement: dense, non-contact point clouds that capture freeform geometry quickly enough to keep takt time or MRO turnaround viable.
A scanner with a large depth of field, such as the 650mm scanner depth offered by INSVISION’s industrial 3D scanner, reduces the number of repositioning moves required to cover a large freeform surface. That directly cuts the labor hours tied to data acquisition.
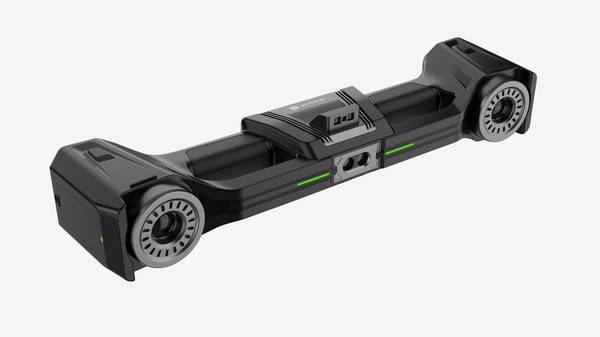
When routing a quote, I look at part size and site freedom first. For large aerospace tooling or composite layup mandrels, the industrial 3D scanner’s 1100mm x 800mm scanning area and 2300mm tracker depth of field provide the working volume needed without constant tracker relocation. For smaller, high-detail implants, the same workflow logic applies but with tighter accuracy requirements.
The industrial 3D scanner’s stated accuracy of up to 0.020mm for the scanner and 0.025mm for the tracker is the figure quality managers typically need to validate against their internal GR&R studies before moving forward.
The routing decision should always tie back to the specific deliverable—GD&T report, reverse-engineered solid, or traceable point cloud—because that deliverable defines the software and reporting burden downstream.
Key Constraints That Define Freeform Scanning Solution Fit
Plain text only, no markdown, 100-180 words.
Pre-sales teams at INSVISION typically route a freeform 3D scanner inquiry through five filtering questions before any demo. These same questions work well for engineering, quality, and procurement staff trying to avoid buying a system that solves the wrong problem.
First, what is the full size range of freeform parts to be scanned? A system configured for small medical device components will struggle with large energy castings. Second, is on-site mobility required? Factory floor and field MRO work demand a different setup than a controlled metrology lab. Third, can markers be applied, or is marker-free capture necessary? Shiny or delicate surfaces often rule out markers.
Fourth, what takt time is needed for batch inspection runs? Lean manufacturing lines cannot tolerate measurement bottlenecks. Fifth, how repeatable must measurements be for high-volume production?
Each constraint links directly to rework, scrap, and quality traceability costs under Industry 4.0 initiatives. Ignoring one constraint during selection creates downstream labor waste that no software upgrade can fix.
INSVISION Freeform 3D Scanning Portfolio Routing Logic
The core routing decision for any freeform scanning task comes down to four constraints: part size, site access, marker conditions, and repeatability requirements. Once those are clear, the right INSVISION configuration becomes obvious. The portfolio is structured around how teams actually work, not around specification sheets.
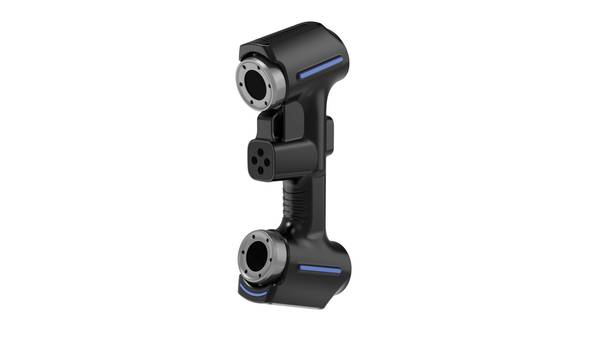
For maintenance crews and field service teams that need to capture freeform geometry on-site, INSVISION offers handheld configurations that travel well and set up quickly. These suit factory floor spot checks, MRO tear-down inspections, and reverse engineering jobs where moving the part to a dedicated lab is not practical. The operator can scan around obstructions and reach into tight areas without repositioning the asset.
This matters when production equipment cannot be taken offline for long.
Large contoured parts present a different problem. Wind turbine blades, aerospace fuselage sections, and marine hull components test the limits of conventional scanning volumes. INSVISION provides tracking-enabled solutions for this category, letting the scanner maintain reference over large working envelopes while the operator moves freely around the part.
The result is continuous freeform data capture without stitching drift accumulating across long surfaces. This is especially relevant for Western aerospace suppliers working to AS9100 documentation expectations.
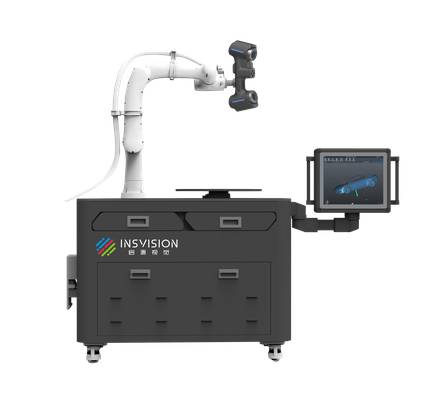
High-batch production lines shift the priority from flexibility to repeatability. When a cell needs freeform inspection to run at takt time, handheld scanning introduces too much operator variability. INSVISION offers automated scanning configurations that hold sensor position and path consistency part after part.
This aligns with lean manufacturing practice: the measurement cycle becomes predictable, and the inspection step stops being a bottleneck. Quality managers can rely on consistent data for SPC trending.
For medical device and aerospace small parts with tight GD&T callouts, INSVISION provides high-precision scanning options suited to complex freeform surface validation. These applications typically involve small features, thin walls, and strict surface profile tolerances. The scanning configuration must deliver dense point data with minimal noise so that inspection software can evaluate against CAD nominal geometry.
The result is reliable first-article and in-process verification without outsourcing to third-party metrology labs.
Across all these configurations, INSVISION supports industry-standard data formats that drop into existing quality and CAD workflows. Engineering teams can bring scan data into PolyWorks, Geomagic, GOM Inspect, or native CAD packages without format friction. That matters in Western manufacturing environments where the scanner is only one part of a broader digital thread connecting design, inspection, and traceability records.
Freeform scanning should integrate with the systems already in place, not force a parallel data silo.
In practice, most plants start with one dominant use case and expand from there. The routing logic is not about finding a single universal scanner but matching the right configuration to the dominant constraint. A field MRO team needs portability. A blade manufacturer needs tracking over large volumes. A production line needs automation and repeatability. A medical device supplier needs precision on small freeform surfaces.
INSVISION covers all four without forcing compromise on data quality or workflow compatibility.
Sample Validation Workflow for Freeform Scanning Fit Confirmation
A structured validation workflow matters when you move from spec-sheet review to an actual purchase decision. Most Western industrial teams don’t need another demo that shows ideal conditions. They need evidence that a freeform 3D scanning solution will hold up against their own parts, their own tolerancing, and their own quality system.
For an INSVISION freeform 3D scanner evaluation, a low-risk path starts with a representative part sample. Send a part that reflects real production geometry — curved surfaces, blended transitions, or areas where conventional touch probing struggles. Have the scan data checked against your ASME or ISO tolerance framework.
This gives you a direct read on whether the point cloud density and dimensional output match what your inspection reports actually require, rather than what a generic benchmark suggests.
Next, pull the scan output into your existing QMS and CAD environment. Check file compatibility, data structure, and whether the mesh or point cloud moves cleanly into your review workflow. If your team already works in a specific inspection software or PLM system, test that handoff before committing to a broader rollout. This step catches integration friction early.
Finally, run a simulated on-site workflow using a second test part. Let your own operators handle setup, scanning, and data export under normal shop-floor conditions. Observe where training time concentrates and how the equipment fits into your current production or inspection sequence.
For teams evaluating creaform ametek freeform 3D scanner alternatives, this kind of structured trial is the real risk-mitigation step. It keeps the decision tied to your part geometry, your quality standards, and your operators — not a vendor’s polished presentation.
INSVISION supports this validation approach without overstating performance claims, which is what a procurement team should expect from any serious industrial scanning supplier.
Actionable Freeform 3D Scanner Pre-Qualification Checklist
Plain text, no markdown, 100–180 words, operational checklist angle, Western industrial buyer language.
Before comparing another spec sheet, run this checklist with your engineering, quality, and procurement teams. It shifts the conversation from scanner features to operational fit, which is where most evaluation time gets wasted.
Start with part size range and freeform feature complexity. If your work mixes small castings with large aerospace skins, confirm the scanning area and depth of field support both without constant repositioning. Required measurement tolerance comes next. Align this against your industry standards, not a generic accuracy claim.
A first-article inspection on a turbine housing and a CAD comparison on a composite layup do not demand the same workflow.
Then address mobility and site access. Shop floor, metrology lab, or field MRO work will determine whether you need a tracker-based setup or a compact scanner-only configuration. Marker application feasibility matters more than many teams admit. Glossy, dark, or delicate surfaces may make targets impractical, so confirm the scanner’s behavior on unmarked geometry.
Check batch volume and takt time targets. Low-volume rework is different from inline repeat inspection. Finally, review your existing software ecosystem and the operator skill level you can actually staff. A tool that demands a dedicated programmer will stall in a lean cell.
Use this checklist as your internal pre-qualification gate when researching Creaform Ametek freeform 3D scanner solutions and comparable INSVISION configurations. It helps engineering, quality, and procurement align on operational constraints before vendor demos begin. The result is a shorter evaluation cycle and fewer mismatched purchases.
Hangzhou Insvision Technology Co., Ltd.
Address: Building 1, No. 1399 Liangmu Road, Yuhang District, Hangzhou, Zhejiang 311121, China
Copyright © Hangzhou Insvision Technology Co., Ltd. All rights reserved.
Copyright © Hangzhou Insvision Technology Co., Ltd. All rights reserved.